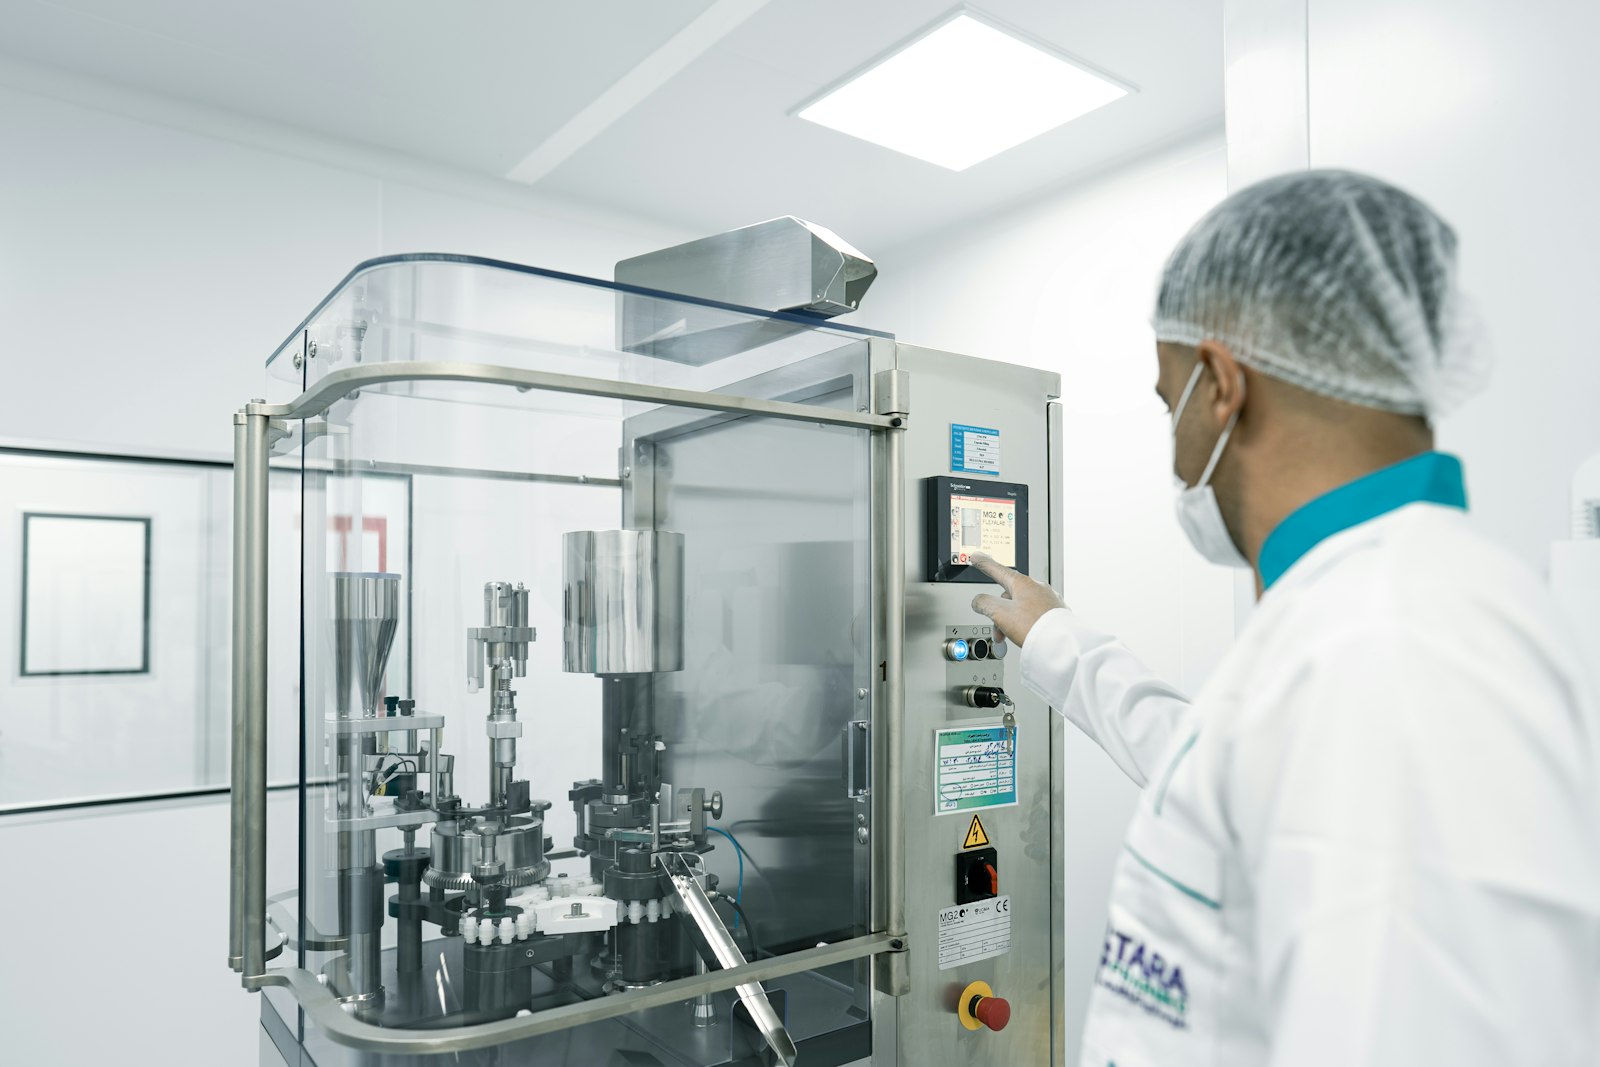
Picture a new tablet press. The supplier runs a factory acceptance test with your engineers watching, every interlock is tried, every alarm is triggered. Two months later the same tests are run again on site, this time under an OQ protocol, by a different team, with the same results. Nobody learns anything new the second time, but it takes two weeks and holds up the start of production.
It does not have to work that way. EU GMP Annex 15 has allowed FAT and SAT results to support qualification since its 2015 revision, and ISPE's commissioning and qualification guide is built around the same idea. The catch is that leveraging only works if it is planned before the FAT, not argued for after it.
What Annex 15 says
The relevant text is short. Where appropriate and justified, documentation review and some tests can be done at the FAT or other stages without repeating them on site at IQ or OQ, provided it can be shown that the functionality is not affected by transport and installation. Three conditions are hiding in that sentence: it must be appropriate, it must be justified in writing, and transport and installation must not change the result.
What can usually be leveraged
- Software and control logic tests, such as sequence, recipe handling, alarms and interlocks, where the same PLC program and HMI are installed on site without change.
- Document checks, such as material certificates, weld logs, drawings and software versions, reviewed once and referenced in the IQ.
- Component-level functional tests that do not depend on site utilities.
What generally cannot be leveraged are tests that depend on the installation itself: utility connections, calibration of installed instruments, performance with site steam, water or air, and anything affected by how the equipment was moved and set down.
What has to be in place
For a FAT result to stand in for an OQ test, it needs to have been produced with the same discipline you would expect on site:
- A test protocol approved before execution, including by your quality unit where the tests support GMP decisions.
- Calibrated test instruments, with the certificates attached.
- Results recorded at the time, signed and dated, in line with good documentation practice.
- Deviations raised, assessed and closed, not fixed quietly and re-run.
- Traceability from each test to the user requirement it verifies.
- Configuration control, so you can show the software and hardware tested at FAT are the ones installed on site.
Where the SAT fits
The site acceptance test confirms that the equipment arrived and was installed as it left the factory, and that it works with your utilities. A short, focused SAT can confirm that the software version and key settings are unchanged since the FAT, which is the evidence you need to say transport and installation did not affect the leveraged tests.
Writing it down
The justification normally lives in the validation plan or the qualification protocol. For each leveraged test, list the FAT or SAT reference, why the result is still valid on site, and who reviewed it. The OQ report then refers to that evidence instead of repeating it.
Done this way, the on-site OQ becomes shorter and more interesting. It concentrates on the things that could only be tested on site, which is where problems are actually found.

 GAMP Services Limited 2026. All Rights Reserved.